 Jiu Ju Magnetizer

Why Can’t I Get My New Tooling Aligned Right? Three Pitfalls to Avoid When Quickly Changing Setups with Magnetizing Fixtures
End-to-End Solution for Magnetization Automation
Automated Magnetic Charging Integrated Solution
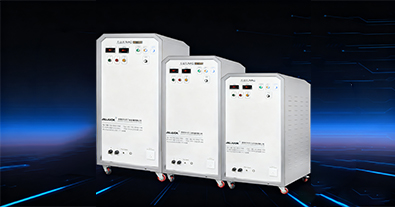
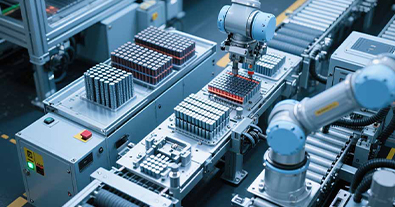
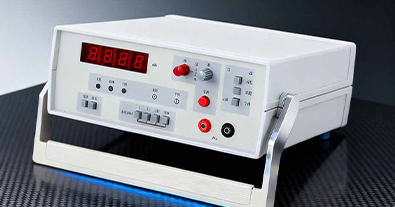
Q1: Every time I change the product specifications, the magnetization becomes unstable, and it takes half an hour of adjustment to get it back to normal. What’s causing this problem?
A: In 90% of cases, the problem lies with the positioning of the production fixtures. The positions of the coils and fixtures vary depending on the product, and many factories rely on visual alignment or marking lines with a marker pen during changeovers—this level of precision is simply insufficient. If the air gap between the coil and the magnet is off by just five threads, the discharge energy coupling efficiency can drop by more than 10 percent. Standardize changeovers by doing three things: Make a positioning plate for each set of jigs that uses pins andpositioning holes to achieve quick alignment, eliminating the need for manual adjustment. After a changeover, run the test piece through the process three times; proceed to mass production only after consistency is verified. Label each set of tooling with changeover parameters, specifying which product it is configured for, the voltage to use, and the alignment height—new employees can simply follow these instructions.

Q2: After changing the model, the initial magnetization never reaches full capacity, and I have to repeatedly adjust the voltage to find the right value?
A: It’s not a equipment issue; a step is missing in the changeover process. The contact resistance of new fixtures or re-installed fixtures is different from before, so the discharge energy is actually much lower at the same voltage. After a changeover, discharge the system once without installing the magnet. Use an oscilloscope current probe to capture the waveform and check whether the peak current matches the standard value. If it doesn’t, inspect the fixture’s contact surfaces for oxidation or poor contact. These two issues account for the vast majority of cases where the system fails to fully charge during a changeover. Include this step in the changeover operating procedures. Spending an extra two minutes on this check during each changeover is far more cost-effective than spending half an hour later repeatedly adjusting the voltage.
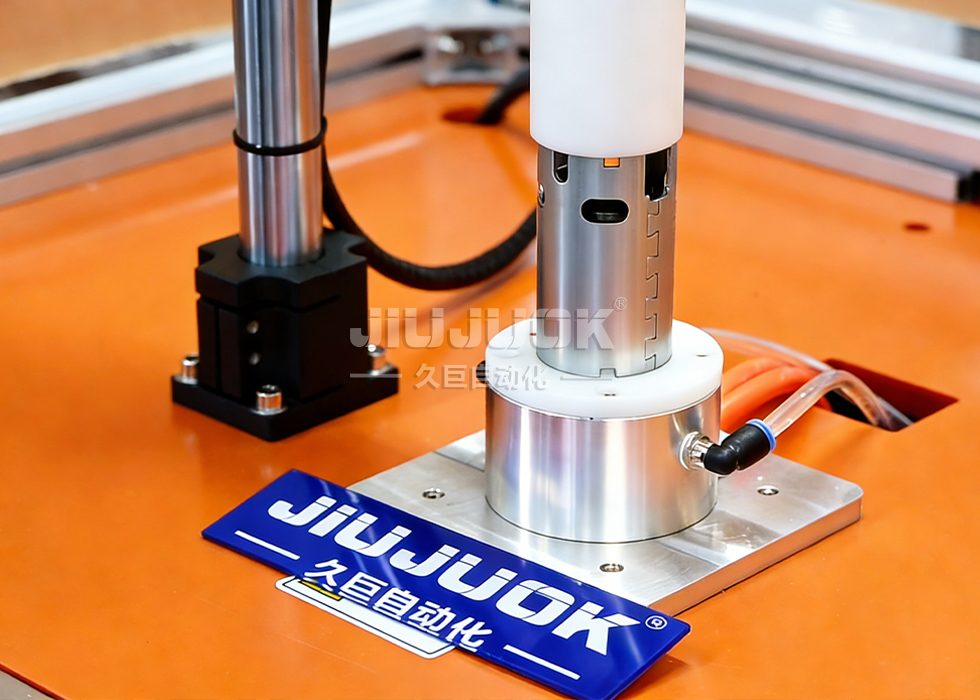
Q3: How do I choose between copper and aluminum fixtures? What are the consequences of choosing the wrong one?
A: Each has its own uses. Copper has good electrical conductivity and is highly efficient at transmitting discharge energy, but it is heavy, making large fixtures difficult for operators to lift; furthermore, copper can be attracted by strong magnets, which is unsafe. Aluminum is lightweight but has poorer electrical conductivity than copper, resulting in slightly higher contact resistance. The standard practice is to use a copper alloy or copper-tungsten alloy for the conductive contact point—limited to an area about the size of a thumb to ensure contact quality—while the main body of the fixture is made of aluminum alloy to reduce weight, thereby balancing efficiency and operational safety. Note that the surface of aluminum fixtures is prone to oxidation, forming a non-conductive oxide layer. Before each shift, gently brush the contact surfaces with a wire brush. If this simple step is skipped, contact resistance can double after a changeover.
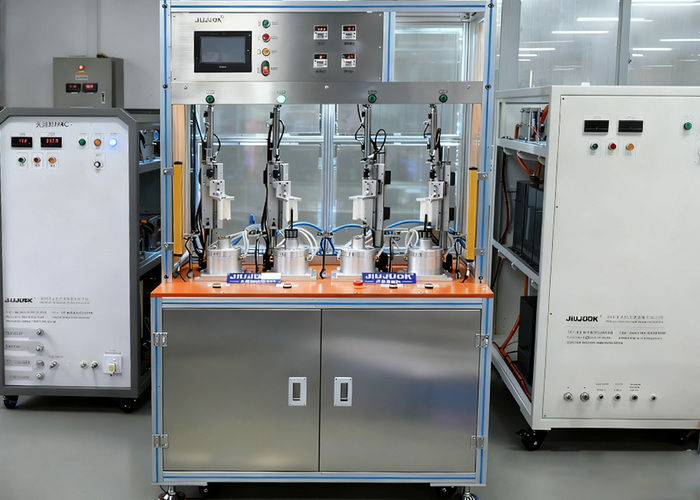
Magnetization of Magnetic Materials
3C Electronic Magnetization
Motor Rotor Magnetization
Car Speaker Magnetization
New Energy Vehicle Industry
Medical Equipment Industry
Other Industries

Jiuju Magnetization 100 Q&A: What Counts as a Defective Magnet
Nov 10, 2026
Defects in permanent magnets go beyond appearance: magn…

Magnetization 100 Q&A: Choosing the Magnet Operating Temperature
Nov 10, 2026
Operating temperature is the core constraint in magnet …

Precise Magnetization Control for AlNiCo Magnets: Case Video
Oct 30, 2026
AlNiCo magnets keep stable flux thanks to a very low te…

How NdFeB Magnets Achieve Stable Magnetism: Case Video
Oct 9, 2026
Stable NdFeB performance requires the right grade, a co…
Magnetization for Magnetic Phone Chargers – Precisely Aligned with Core Magnetic Charging Processes
Nov 13, 2025
Magnetizing magnetic charging heads for phones: matchin…
JIUJU Electronic Magnetizers: Solving Industry Pain Points and Achieving the Optimal Balance of Performance and Cost
Nov 11, 2025
The Jiuju electronic magnetizer balances performance an…
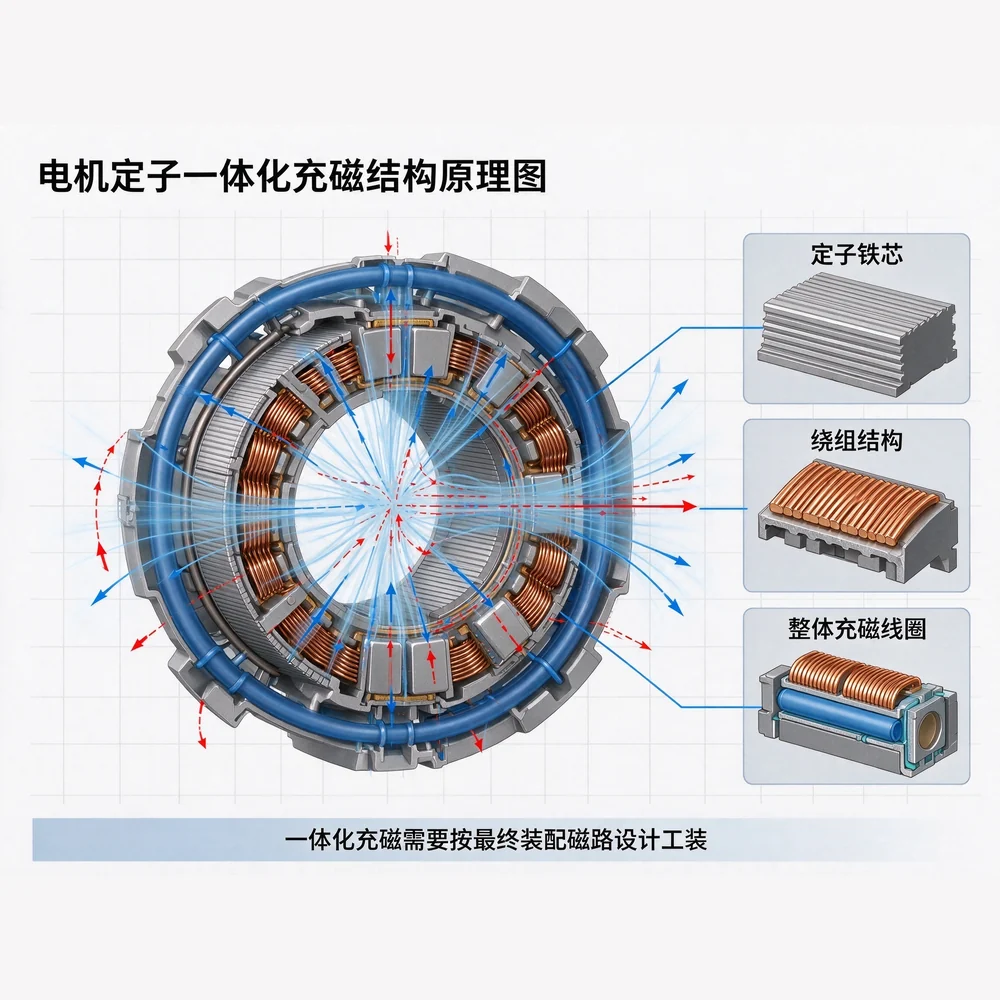
定子一体化充磁成为热点,久巨方案相比单体充磁有哪些利弊?
Nov 20, 2026
两种方案没有绝对优劣,差别在磁化时机。一体化让磁化方向跟着实际磁路走,代价是工装复杂、能量高;单体简单高效,但要防装配二次退磁。
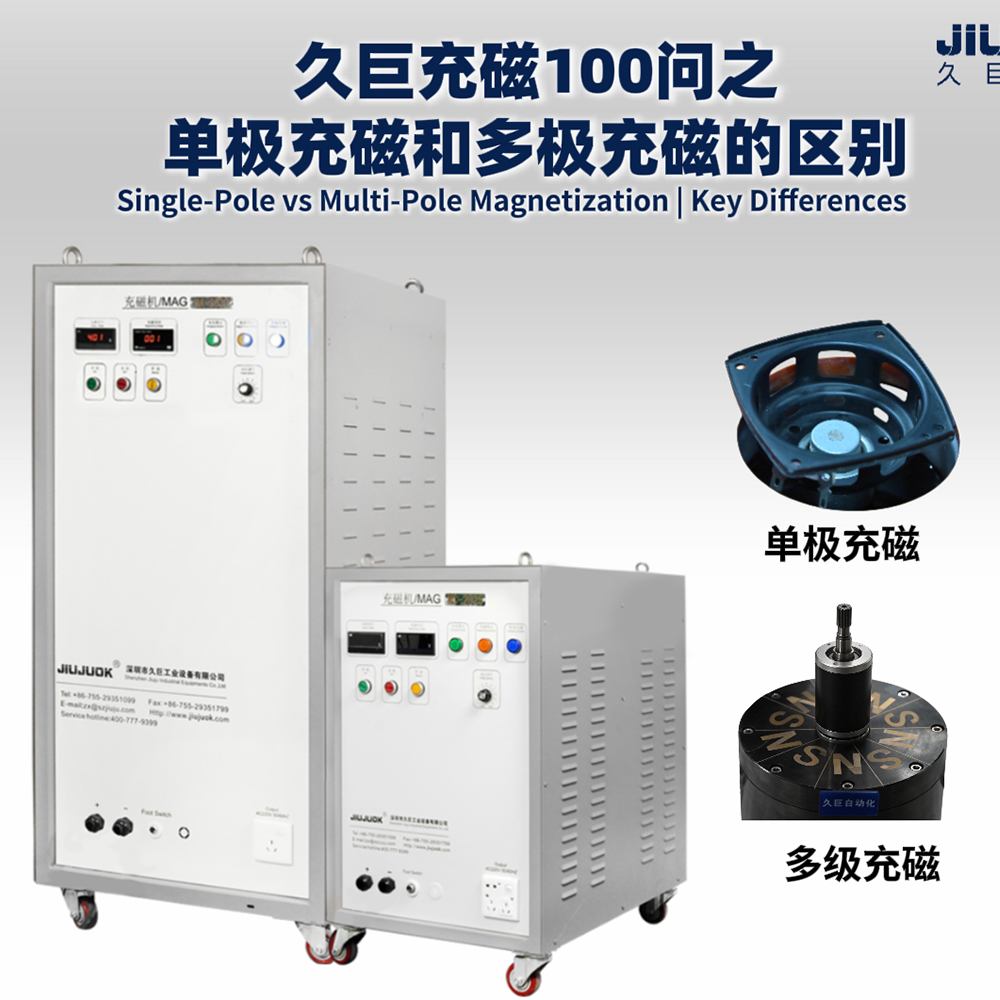
Magnetization 100 Q&A: Single-Pole vs Multi-Pole Magnetization
Nov 10, 2026
This video explains the difference between single-pole …

Video Demonstrating the Magnetization of Jiuju High-Frequency Drivers—Jiuju Magnetizer
Sep 14, 2026
Case video: Video Demonstrating the Magnetization of Ji…

Unusual Noises and Power Loss in Motors? The Root Cause Is an Uneven Magnetic Field—Jiuju Magnetizing Machine
Sep 6, 2026
Motor noise and torque loss often trace back to uneven …

How Critical Is Magnetization in Magnetic Switch Production?
Oct 29, 2026
In magnetic switches, magnetization controls holding fo…

Video Demonstrating Jiuju's Magnetization Process for Antique Speakers—Jiuju Magnetizer
Sep 13, 2026
Case video: Video Demonstrating Jiuju’s Magnetization P…
Video Demonstrating the Magnetization Process for Jiuju Speakers—Jiuju Magnetizer
Sep 10, 2026
Case video: Video Demonstrating the Magnetization Proce…

Why Does the Tip “Stick” to the Screw? A Video Explanation of Magnetization—Jiuju Magnetizing Machine
Aug 2, 2026
Case video: Why Does the Tip “Stick” to the Screw? A Vi…
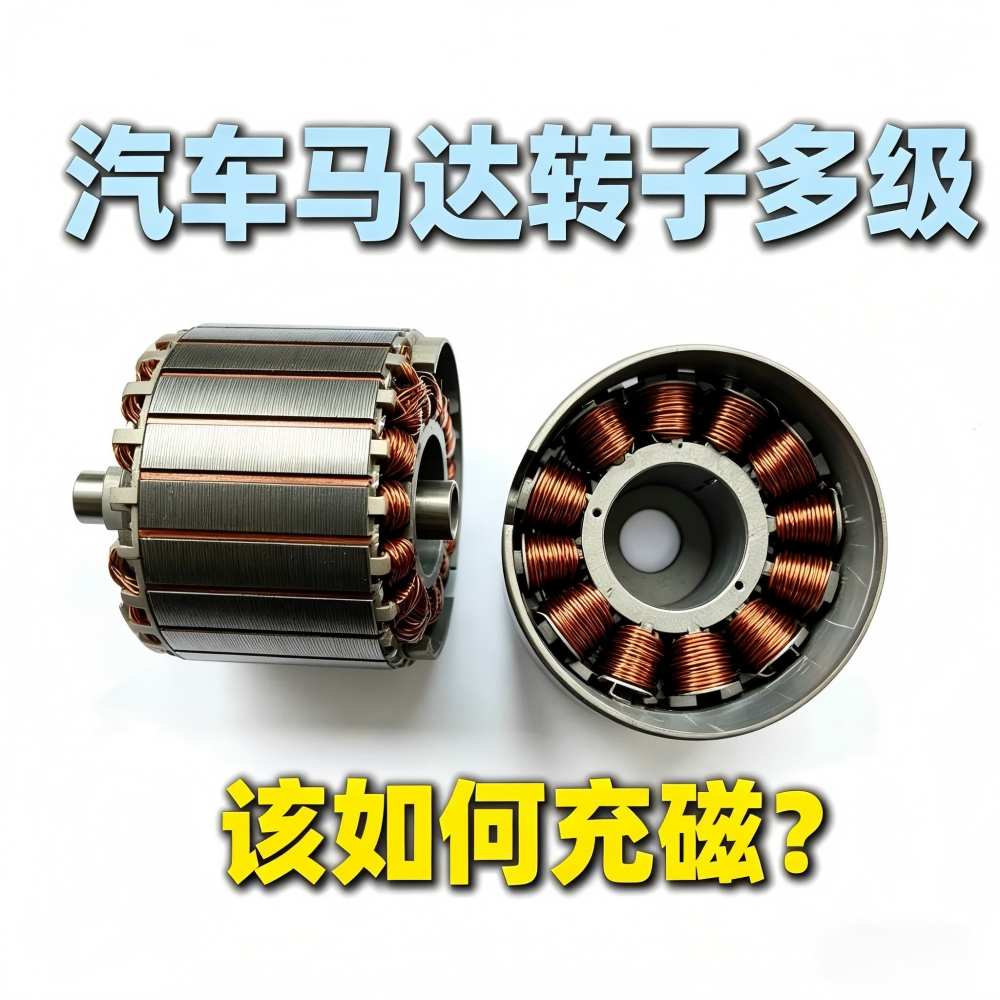
Video on Magnetizing Automotive Motor Rotors—Jiuju Magnetizing Machine
Jul 22, 2026
Case video: Video on Magnetizing Automotive Motor Rotor…

Video Case Study: Magnetizing Machine for Automotive Motor Rotors—Jiuju Magnetizing Machine
Jul 5, 2026
Case video: Video Case Study: Magnetizing Machine for A…

JIUJU Four-Station Motor Magnetizer – A Revolutionary Solution to Enhance New Energy Vehicle Motor Manufacturing Efficiency
Nov 10, 2025
The Jiuju four-station motor magnetizer improves effici…


Video Guide on How to Select a Magnetizing Machine—Jiuju Magnetizing Machines
Aug 8, 2026
Case video: Video Guide on How to Select a Magnetizing …
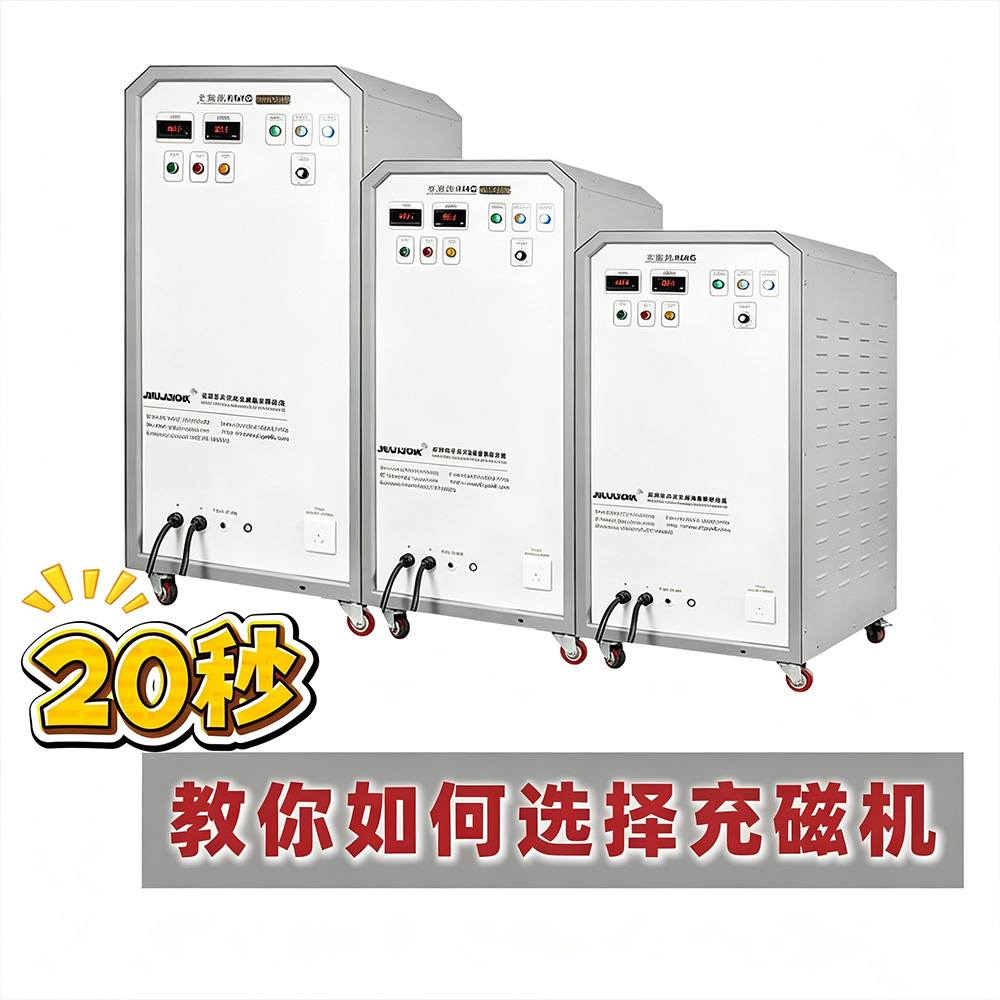
A 20-Second Video Guide on How to Choose a Magnetizing Machine—Jiuju Magnetizing Machine
Jul 21, 2026
Case video: A 20-Second Video Guide on How to Choose a …
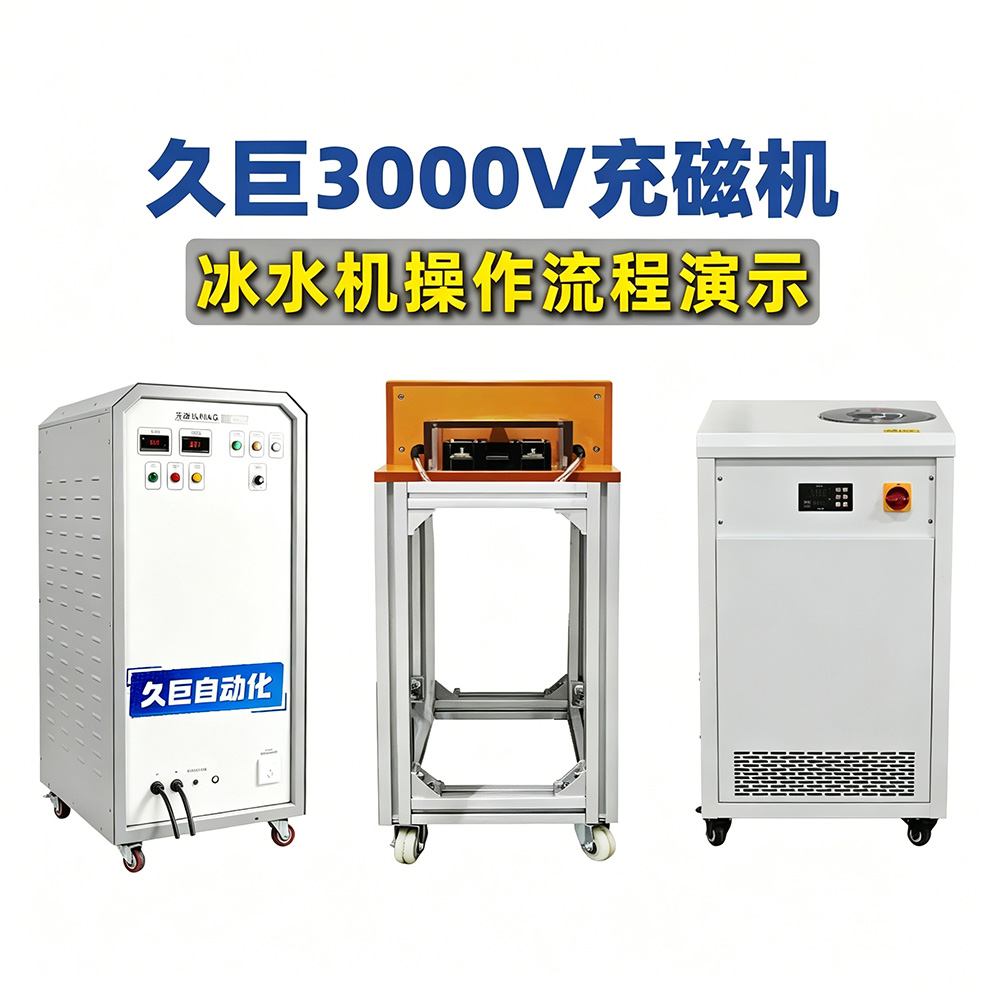
3000V Magnetizing Machine and Chiller Operation Demonstration Video—Jiuju Magnetizing Machine
Jul 3, 2026
Case video: 3000V Magnetizing Machine and Chiller Opera…
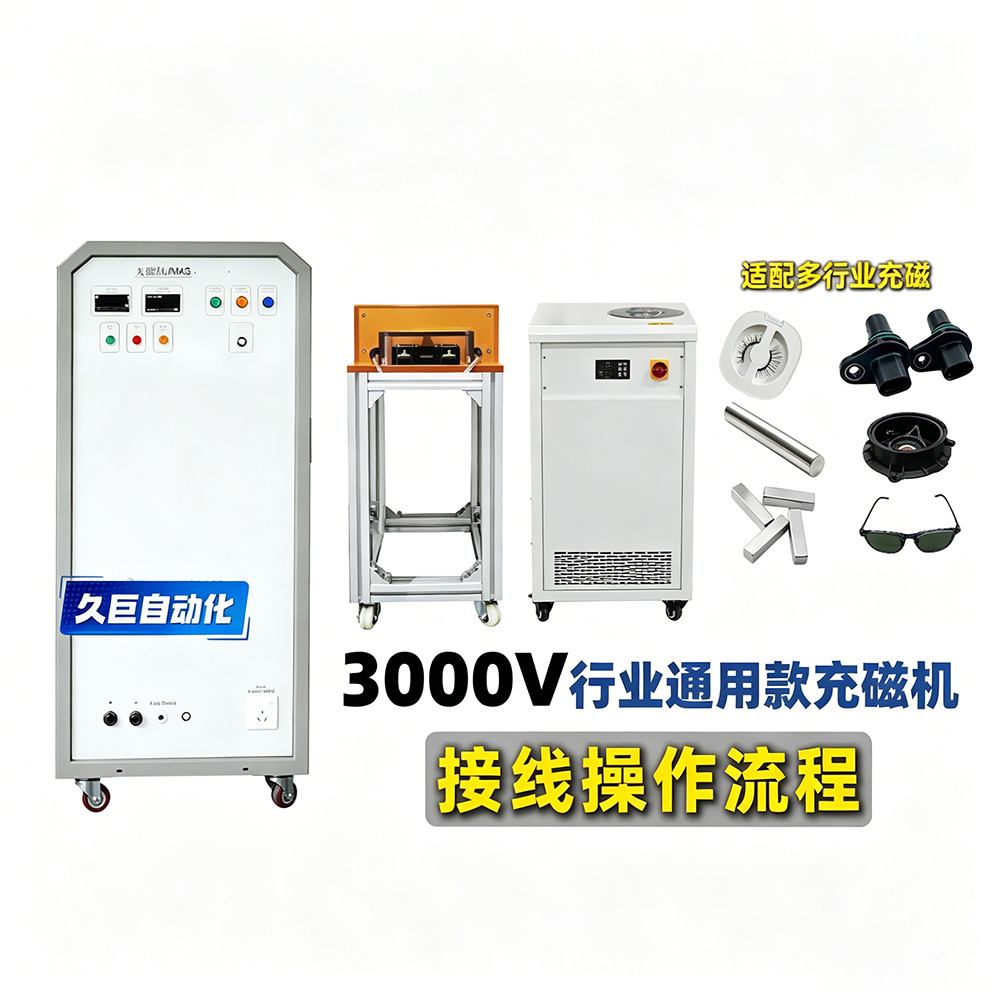
Video on the Wiring Procedure for a 3000V General-Purpose Industrial Magnetizer—Jiuju Magnetizer
Jul 2, 2026
Case video: Video on the Wiring Procedure for a 3000V G…

 English
 Chinese
 Russian
 Vietnamese
 Korean
 Thai
 French
 Spanish
 Japanese
 Hindi
 Bengali
 Portuguese